From pharmacopoeia-grade raw materials to retention samples held one year beyond expiry — every step of production is controlled under a WHO-aligned Pharmaceutical Quality System.
Our workshops are designed, built and operated to China GMP requirements, and in 2026 we once again passed the China GMP on-site inspection. The quality system follows WHO Good Manufacturing Practices (WHO TRS series) for pharmaceutical products.
Following the WHO GMP framework (WHO Technical Report Series), our Pharmaceutical Quality System covers the full product lifecycle — development, technology transfer, commercial production and discontinuation.
Quality manual, SOP system, batch records and training records — every critical operation is written, reviewed and version-controlled.
All deviations are investigated to root cause; corrective and preventive actions are tracked to closure with effectiveness checks.
Changes to materials, equipment, process or documents are risk-assessed, approved and validated before implementation.
Every product undergoes an Annual Product Quality Review — trends in assay, impurities and complaints drive continuous improvement.
No batch ships without QA batch-record review, full QC results review and formal release certification.
Scheduled internal audits of workshops, warehouse, QC laboratory and water system keep the site inspection-ready at all times.
Quality starts before production. Every active ingredient and every excipient that enters our workshops is controlled to pharmacopoeia requirements (BP / USP / EP / CP monographs), from supplier qualification to in-use expiry.
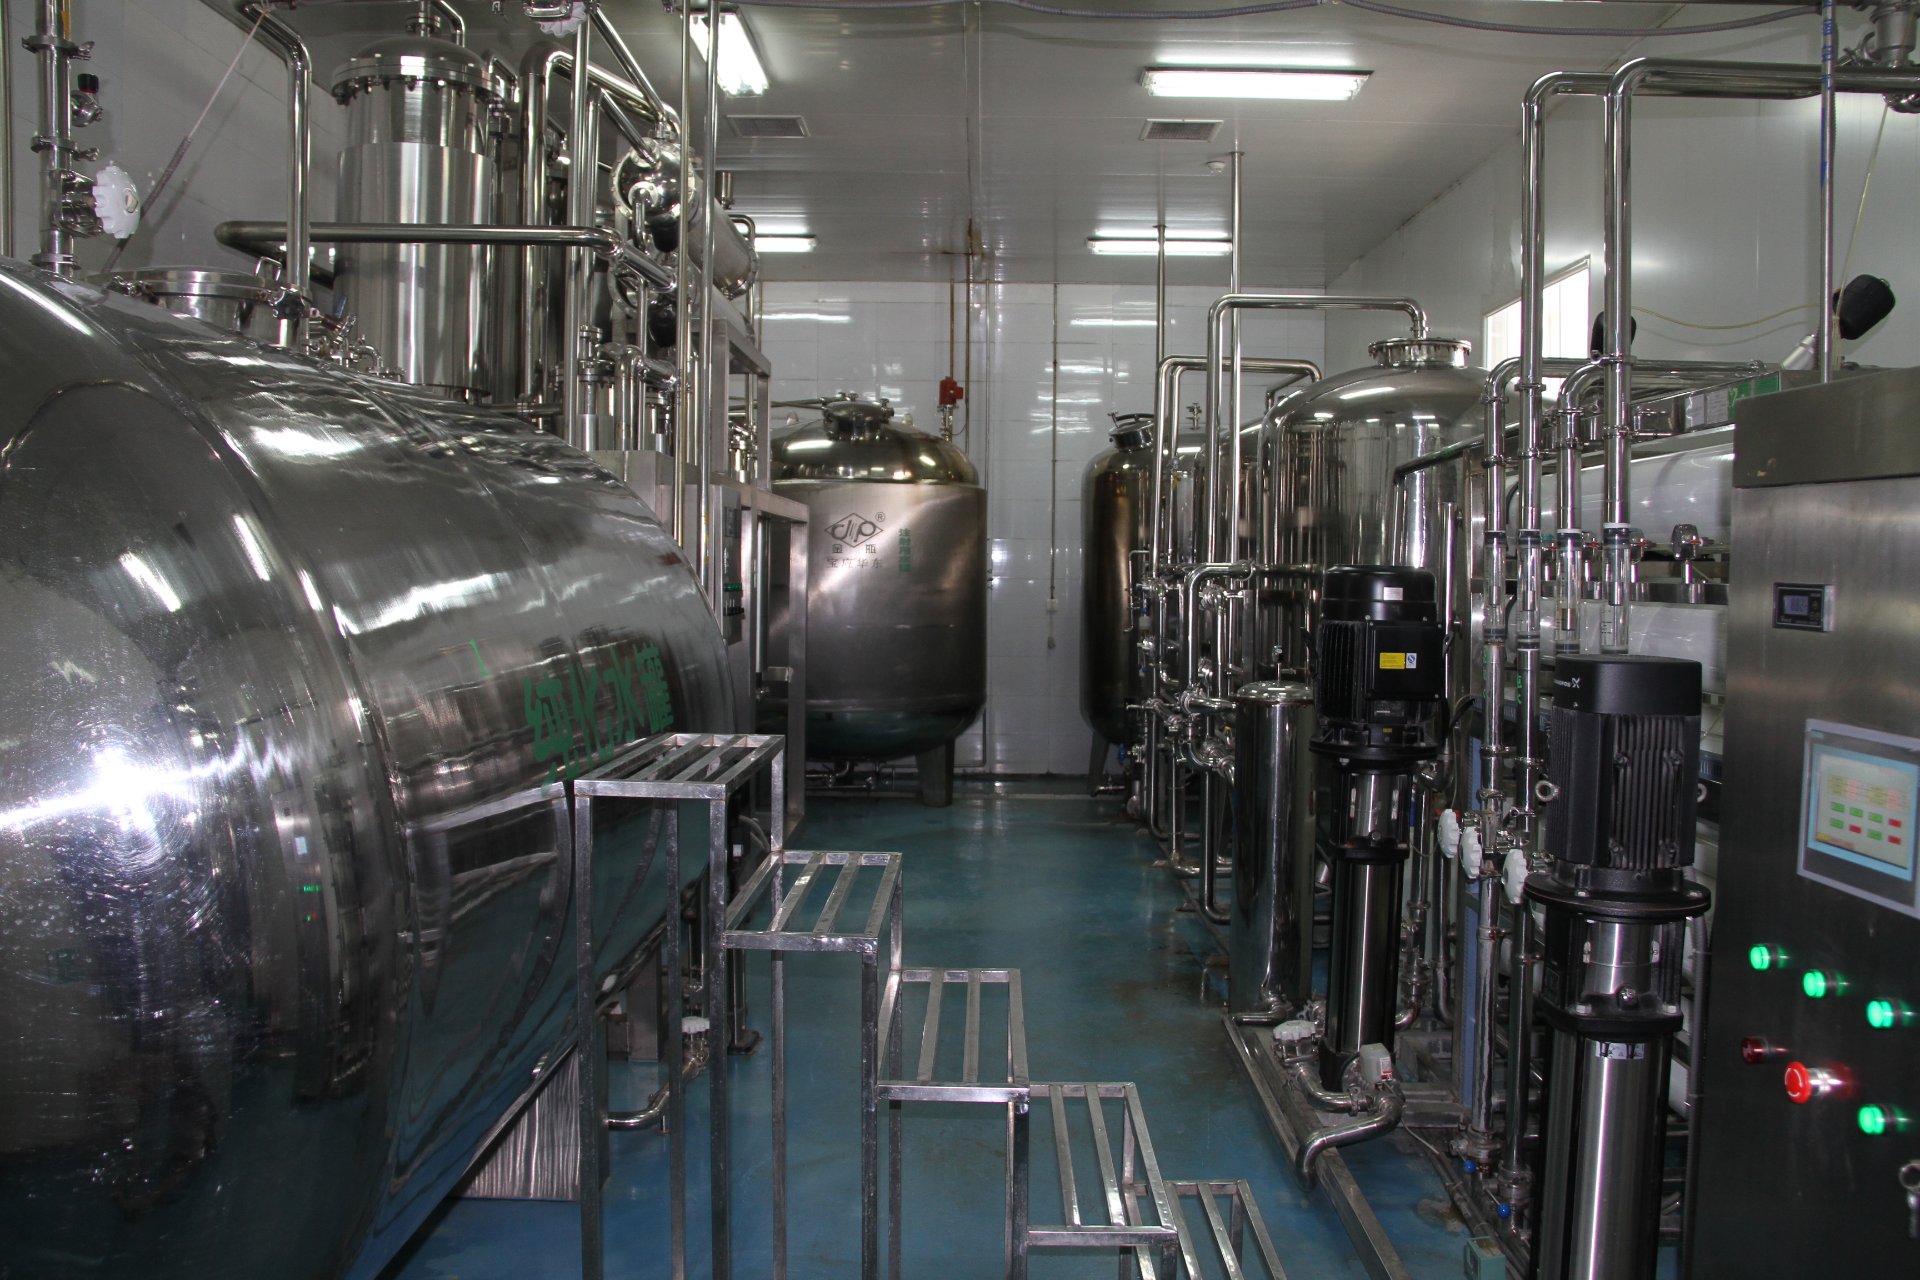
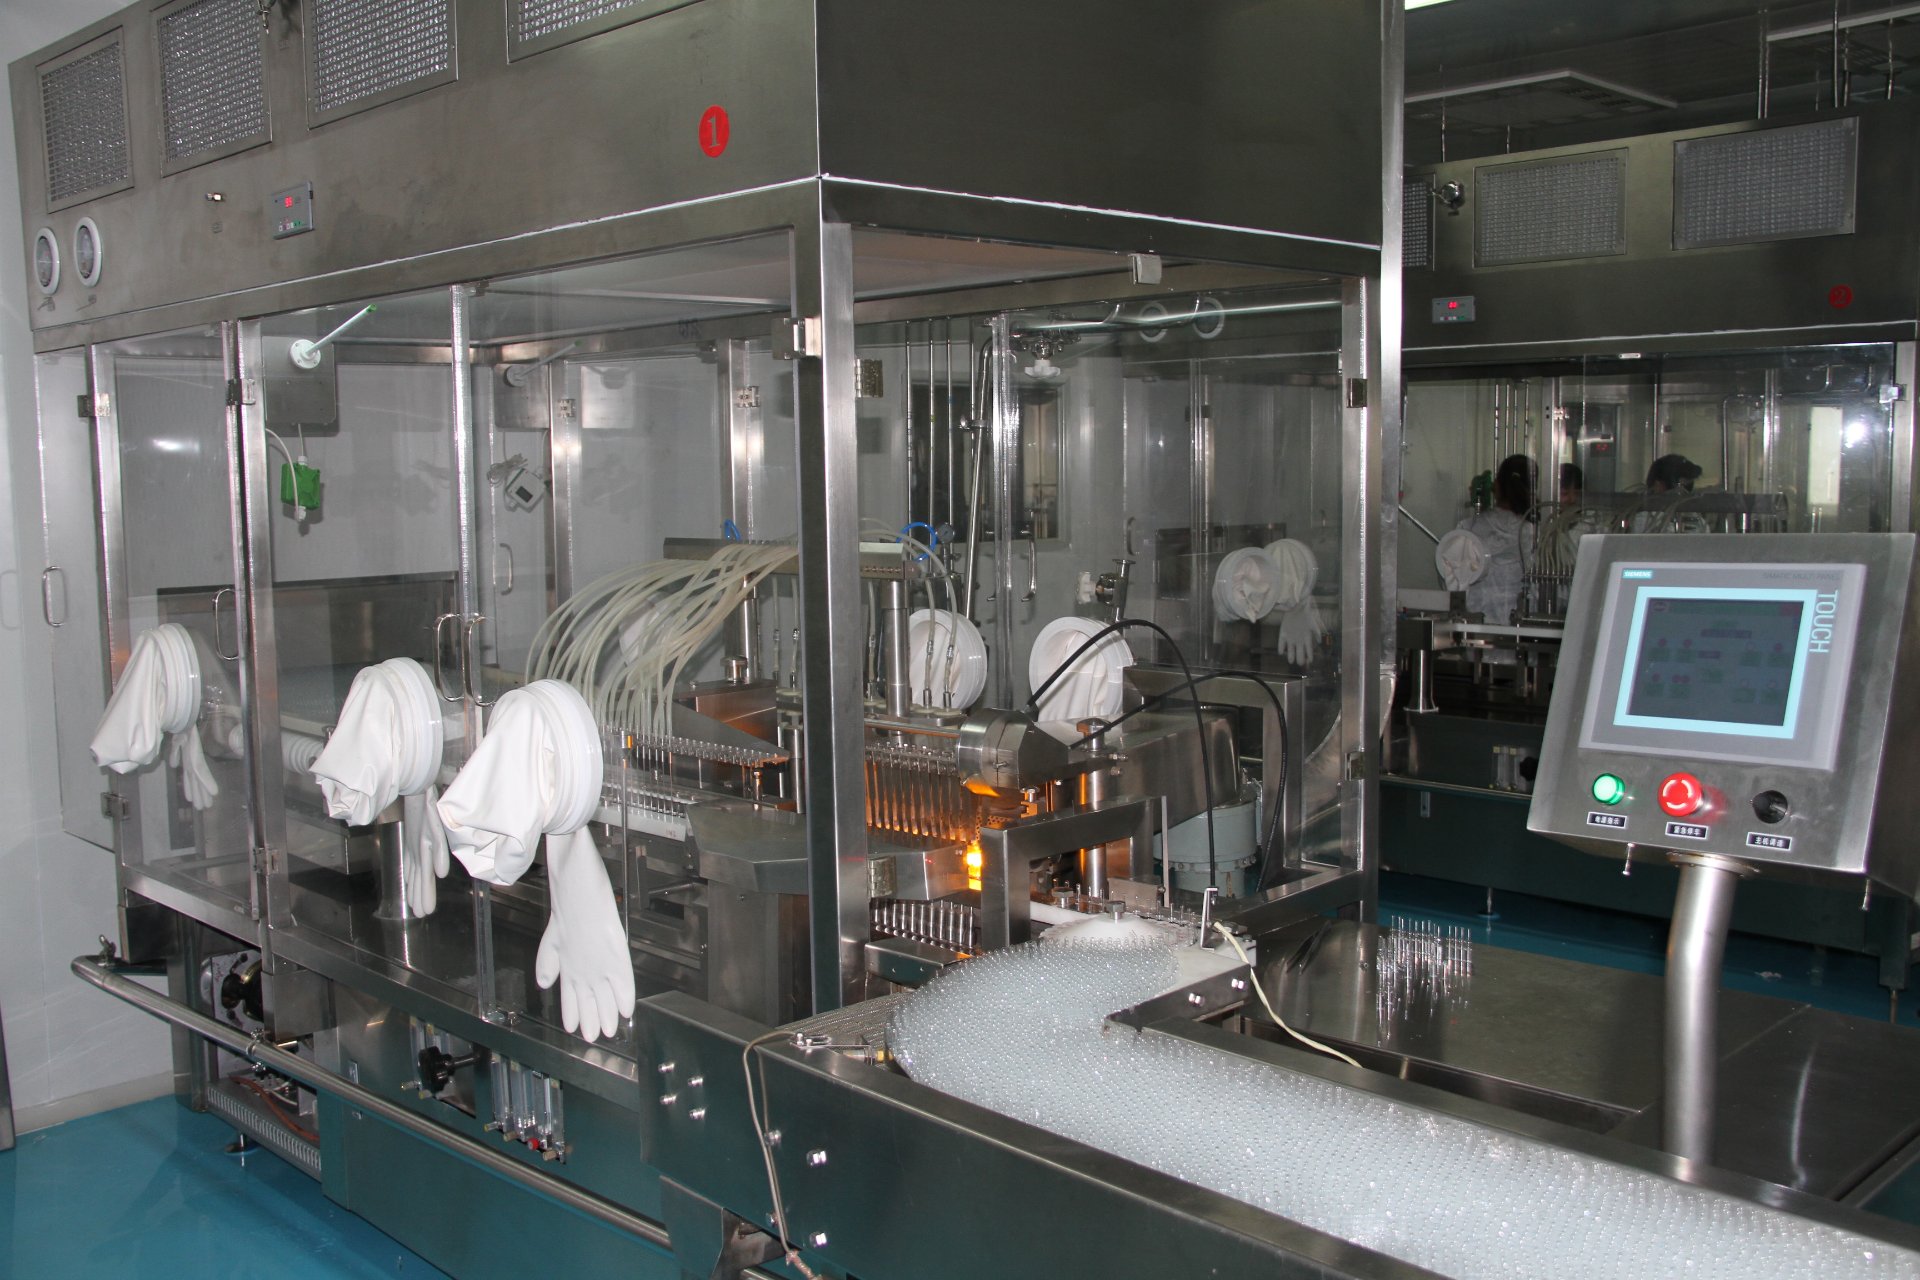
Injection products are only as safe as their water. Our water train produces Purified Water through triple-stage reverse osmosis, then further purifies it by multi-effect distillation to Water for Injection (WFI) quality, fully meeting pharmacopoeia and WHO requirements.
Cleanrooms are classified Grade A to D per WHO GMP. HVAC systems with terminal HEPA filtration maintain a positive-pressure cascade, controlled temperature and humidity; personnel follow qualified gowning procedures, and the environment is monitored for particles and microbiology on a defined schedule.
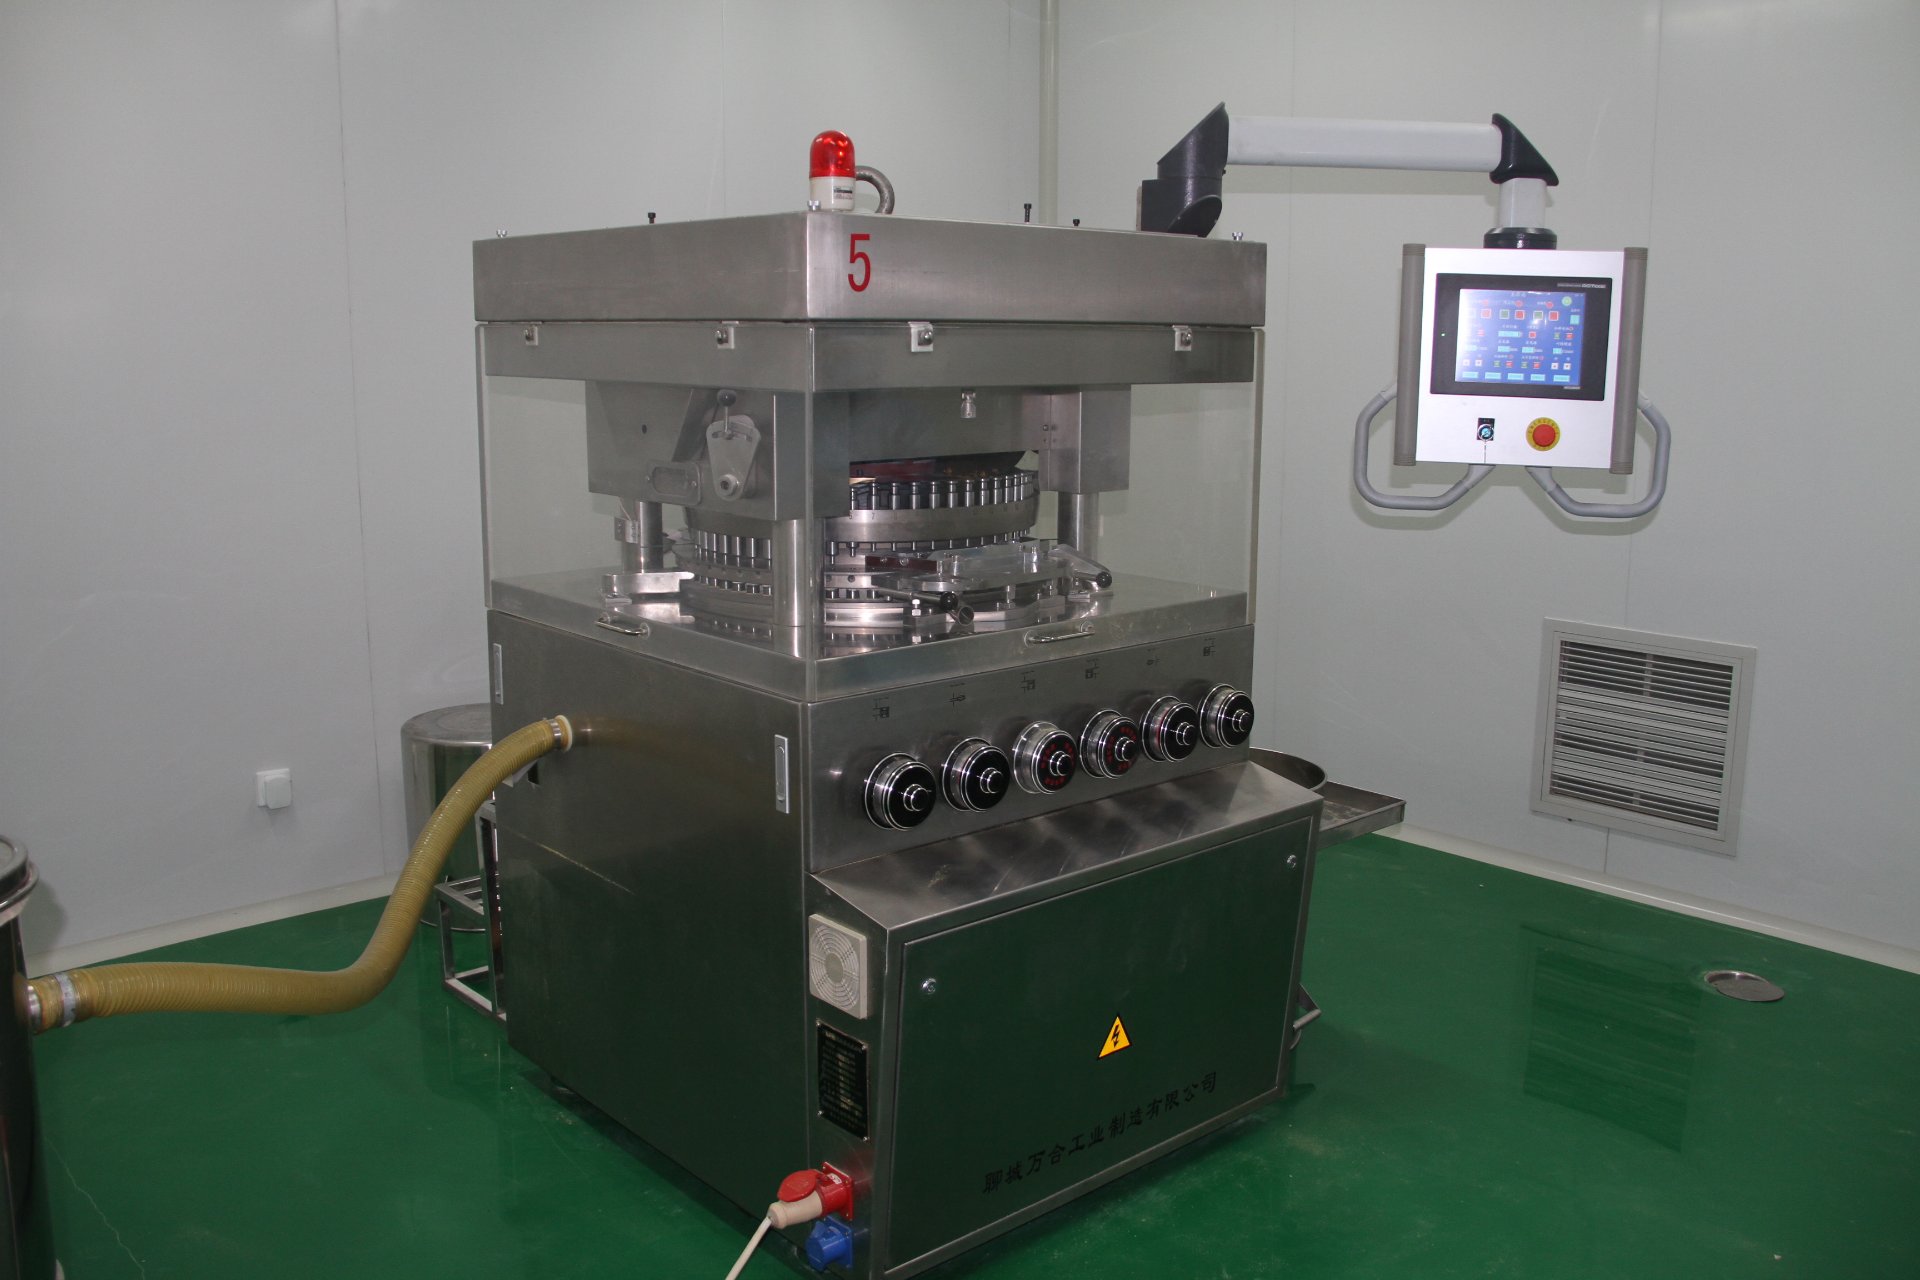
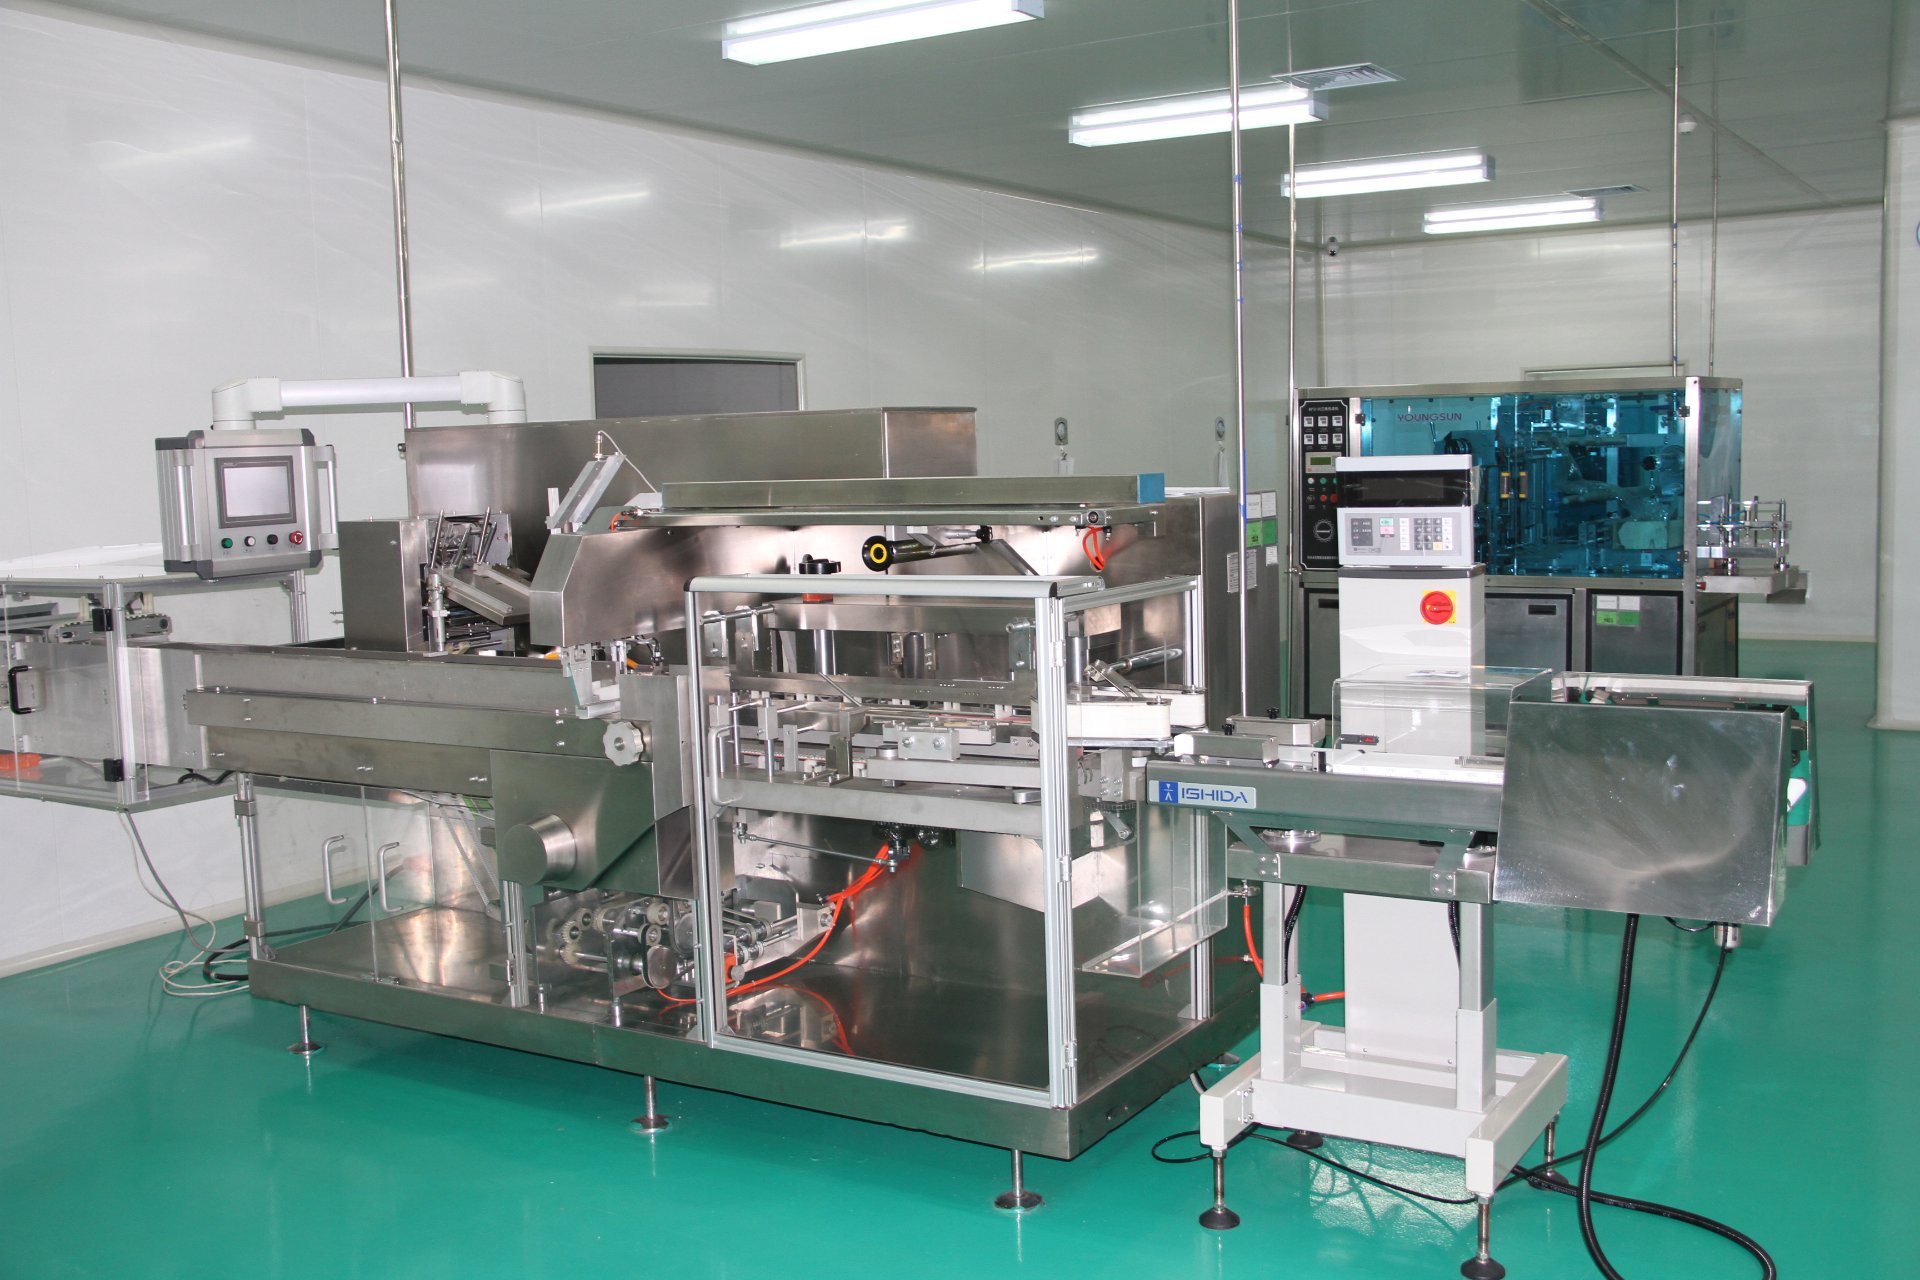
HEPA-filtered air supply with ≥10 Pa positive-pressure differential between adjacent grades, protecting the product flow direction.
Airborne particles, settle plates, contact plates and personnel monitoring on a WHO-defined schedule with alert & action limits.
All operators trained and qualified in aseptic behaviour and cleanroom gowning before entering production areas.
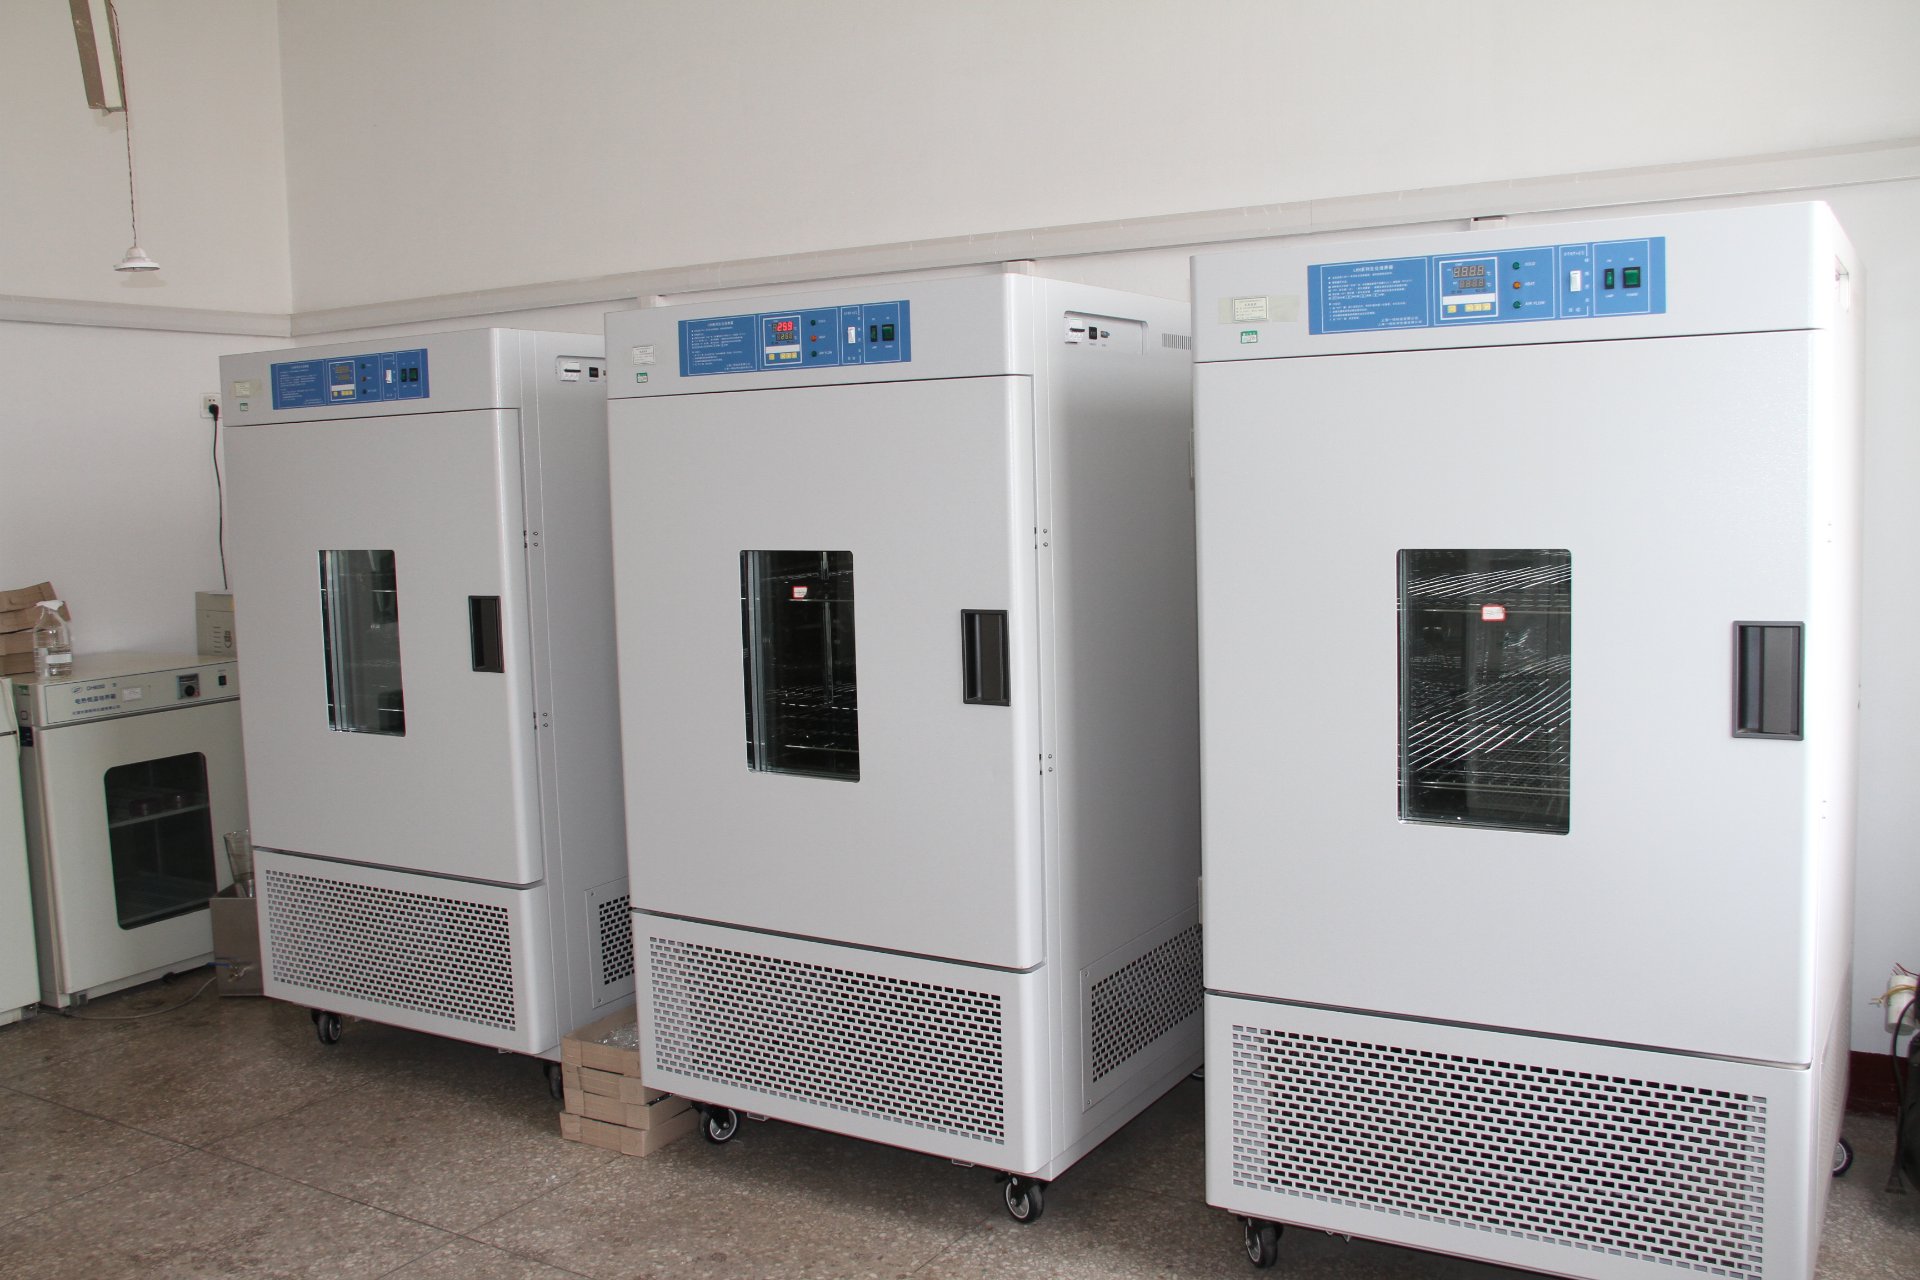
We keep retention samples of every commercial batch in controlled storage until one year beyond the product's labelled expiry date. If any question arises in the market, the exact batch can be re-examined against the original full test panel.
GMP certificates, water system validation summaries, stability data and quality agreements are available for your regulatory submissions. On-site and remote audits are welcome.

 Sinophare Biotech